Top Solar Ground Mount Factories in China Worth Knowing
2026-09-01
The solar ground mount market in China is crowded, but only a handful of factories truly stand out for engineering, scalability, and supply-chain reliability. If you’re sourcing racking systems for utility-scale or commercial projects, knowing which manufacturers actually deliver—rather than just promise—can save months of headaches. In this roundup, we’ve cut through the noise and profiled the facilities worth your attention, including Topfencesolar, a name that keeps surfacing for its practical designs and consistent lead times.
Factories That Quietly Power the Solar Boom
Behind the gleaming solar panels that dot rooftops and stretch across desert plains, a quieter revolution hums inside unassuming industrial buildings. These are the factories where raw quartz sand is transformed into high-purity polysilicon, where hair-thin wires slice silicon ingots into shimmering wafers, and where automated lines assemble thousands of cells per hour. While much of the public attention goes to installation crews and final panel brands, the steady expansion of these upstream facilities is what keeps the global solar supply chain from buckling under skyrocketing demand.
What sets the current wave apart is how rapidly the production floor itself has evolved. Older plants relied on batch processes and manual inspection; newer ones run continuous chemical vapor deposition reactors that can churn out polysilicon around the clock, with machine vision systems flagging micro-cracks that the human eye would miss. A single modern factory in China’s Xinjiang province or Germany’s solar valley can produce more wafer capacity in a month than an entire national industry did a decade ago. That scale has driven costs down so sharply that solar is now the cheapest electricity source in history—yet it also means a single furnace maintenance hiccup or a shortage of specialty graphite can ripple across three continents within weeks.
Labor in these factories tells its own story. The workforce is no longer dominated by low-skill handlers but by process engineers, data analysts, and robotics technicians who monitor vast cleanrooms from control rooms packed with dashboards. Many plants operate on a “lights-out” shift where only a skeleton crew remains overnight, tending to machines that never sleep. For regions that lost traditional manufacturing jobs, these factories offer a different kind of employment—one tied to clean energy’s relentless march. Yet the work is often invisible to the public, hidden behind security fences and nondescript warehouse exteriors. That invisibility belies the fact that every silent wafer leaving the production line carries the weight of the energy transition on its thin, brittle surface.
A Closer Look at Mounting Systems Built for Extreme Weather
Most off-the-shelf racking fails not from steady pressure but from cyclic loading. A mounting system for extreme weather has to tolerate repeated micro-impacts, thermal expansion mismatches, and salt spray that eats standard galvanization within a few seasons. We've seen aluminum rails crack near the bolt slots after one winter in the Upper Midwest, simply because the anodized layer was too thin to handle freeze-thaw abrasion against the module frame. That's why serious designs use thick-walled 6000-series extrusions with isolated stainless fasteners and EPDM gaskets rated for -40°F to 185°F.
Wind tunnels and snow-load maps only tell part of the story. A mounting system needs to be tested as an assembly—not just individual brackets—under uplift, downforce, and lateral shear. The best performers use triangulated cross-bracing rather than relying on roof penetration friction. In hurricane-prone coastal zones, that often means fewer but deeper attachments, each rated for over 2,000 pounds of pull-out, and a rail span trimmed by 30% compared to standard residential installs. If the system can survive a hundred rapid pressure changes between 50 and 120 psf without loosening a single bolt, it's probably built for real weather, not just the datasheet.
The Engineering Culture Behind Reliable Ground Mounts
Reliability in ground mounts rarely comes from a single clever design. It grows out of a team habit of treating every field failure as a design input, not a blame event. When a post shifts in high wind or a clamp loosens after thermal cycling, the data gets pulled into the next revision meeting. Engineers and installers sit in the same room, mark up the failed part, and argue about root cause until the fix makes sense to the person turning the wrench.
Prototypes get abused on purpose. A new mount might be driven into rocky fill, sandy loam, and clay on the same afternoon, then left under load for a season before anyone signs off. Strain gauges on the welds and torque checks on the bolts happen after freeze-thaw cycles, not just in a clean lab. That kind of testing costs time, but it's cheaper than discovering a systemic weakness after three hundred arrays are already in the ground.
The culture also keeps the feedback loop short. Field crews photograph every installation problem, and those photos show up in the next design review without being filtered through a marketing lens. Designers are expected to spend time on site at least twice a year, often with a torque wrench in hand. Over time, this creates a shared vocabulary between the people who draw the mounts and the people who stand on them, which is where dependable engineering actually comes from.
What Separates Export-Ready Manufacturers from the Rest
The gap between a factory that wins repeat international orders and one that loses buyers after the first shipment rarely comes down to machinery or price alone. Export-ready manufacturers build their operations around verifiable standards: they hold certifications that buyers in target markets actually recognize, maintain calibration logs that can be pulled up during an audit, and design packaging that survives multi-week ocean transit without damage claims. Compliance here is not a checklist for the sales team but a daily habit on the floor, so when an inspector walks in unannounced, the line keeps running instead of stopping to hide nonconforming stock.
A second, less obvious filter is financial and communicative stamina. Shops that export successfully quote lead times that include port congestion and customs holds rather than hoping for the best, and they have multilingual staff who can answer a technical question at 11 p.m. in the buyer's time zone without losing details in translation. Their payment terms accept 60- or 90-day cycles because their working capital is structured for it, which quietly removes the biggest friction point in cross-border deals: the fear that a supplier will go silent once the deposit clears.
The clearest differentiator, though, appears when problems arise. Export-ready manufacturers send a corrective action report before the buyer has to ask, with photos, root cause analysis, and a containment plan already attached. They treat a delayed container or a minor defect not as a shameful secret but as a chance to prove their systems work under stress. Buyers notice the difference immediately, because a supplier that volunteers bad news early is far more reliable than one that only shares good news and forces the client to discover the rest at the destination port.
Supply Chain Advantages You Won't Find in Marketing Brochures
Most procurement teams chase cost per unit or lead time dashboards, but the quieter advantages live in how a supplier behaves when things break. A vendor who will reroute a partial shipment on a Friday afternoon because your production line stalled can’t be captured in a brochure. That kind of flexibility comes from years of shared problem-solving, not from a contract clause. It shows up as a warehouse manager who knows your part numbers by heart and flags a pallet that looks short before it ever reaches the dock.
Another overlooked edge is informational. When suppliers trust you, they share early warnings about material shortages, port congestion, or machinery maintenance schedules that will affect deliveries two quarters out. Marketing materials never mention that your best supplier might call you before they call their own sales team. That heads-up can let you adjust orders, pre-buy critical components, or shift production lines while competitors are still waiting for the official delay notice. These are durable advantages, but they only grow through repeated fair dealing and clear communication.
Picking a Factory That Can Scale With Your Pipeline
When you start vetting factories, don't just ask about current capacity—ask how they handled their last three demand spikes. A plant that can scale isn't necessarily the one with the biggest square footage; it's the one with a flexible floor layout, cross-trained workers, and the ability to add a night shift without months of delays. Look for signs of modular thinking: movable assembly stations, quick-change tooling, or a documented process for onboarding temporary staff. If the factory manager starts talking about "hard limits" within the first five minutes, that's a red flag.
Transparency around production data matters more than you might think. A scalable partner will have live dashboards or at least weekly output reports that show where bottlenecks appear when volume climbs. They won't hide behind vague timelines or blame "unexpected issues" repeatedly. Instead, they'll walk you through their workflow and point out exactly which machines or processes become constraints at 80%, 120%, or 200% of your current order size. This kind of honesty lets you plan inventory and lead times without nasty surprises.
Finally, consider geographic and logistical weaknesses that only reveal themselves under growth. A factory in a remote inland area might offer attractive per-unit pricing now, but when you need to double shipments, trucking delays or limited carrier options can eat up all those savings. The best scaling partners are often near major ports or freight hubs, or they have experience coordinating multiple sub-factories to balance load. Ask for references from clients who grew rapidly with them—not just ones who stayed at the same volume for years.
FAQ
Arctech Solar, Antaisolar, Clenergy, and Mibet stand out for their large production capacity, consistent export track record, and engineering teams that support utility-scale projects across Asia, the Middle East, and Latin America.
Most supply fixed-tilt racking, adjustable-angle mounts, and single-axis or dual-axis trackers. Materials usually include hot-dip galvanized steel for structural parts and aluminum alloys for clamps and rails, with options for pre-assembled components to speed up field installation.
Reputable factories run automated cutting, punching, and welding lines, then apply batch testing for weld strength and coating thickness. Many hold ISO 9001 and ISO 14001 certifications, and some also do wind tunnel testing or salt spray tests for coastal projects.
Buyers typically point to lower per-watt structural costs, the ability to adjust designs quickly for different terrain, and shorter lead times. Large factories can also bundle steel procurement in-house, which keeps material costs and shipping volumes predictable.
Look at the number of completed utility-scale installations, especially in similar soil and wind conditions. Ask for detailed drawings of the pile or foundation connection, galvanizing thickness reports, warranty terms, and whether the factory assigns an engineer during the first installation phase.
Yes, many provide site-specific design based on geotechnical reports, offering ground screws, driven piles, or concrete ballast foundations. Adjustable leg heights and slotted connections help accommodate slopes without excessive grading.
Jiangsu, Fujian, Hebei, and Tianjin host many of the major manufacturers because they sit close to steel mills, coating facilities, and container ports. This clustering shortens raw material delivery and export logistics.
There has been a clear shift from basic fixed structures toward smarter single-axis trackers with backtracking algorithms and higher wind resistance. Designers also focus on reducing steel weight per megawatt and simplifying field assembly to cut labor time.
Conclusion
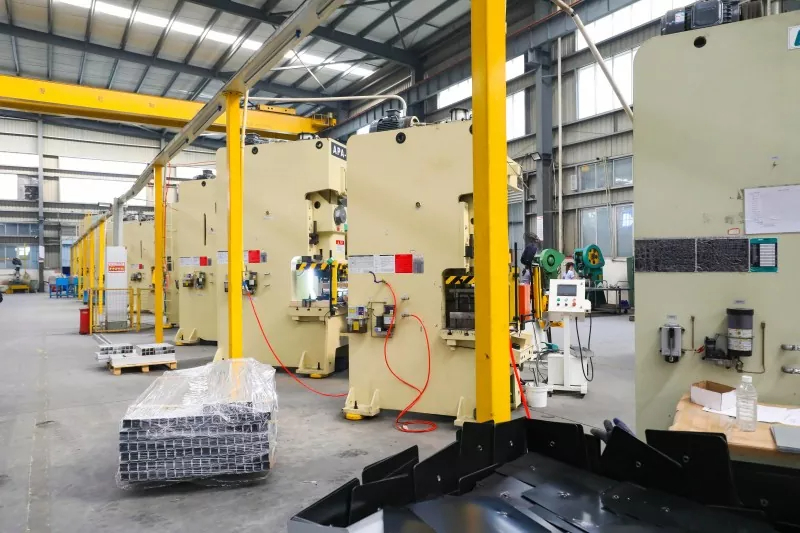
China’s ground-mount sector isn’t a monolith, and the factories worth knowing are rarely the loudest at trade shows. Many of them sit in industrial parks across Jiangsu, Zhejiang, and Hebei, running 24-hour shifts to feed utility-scale projects on four continents. What separates them isn’t a glossy catalog but how they handle extreme weather. Walk through a serious plant and you’ll see full-scale racking assemblies bolted to hydraulic test rigs, simulating typhoon gusts, heavy snow, and cyclic wind uplift. The engineering culture shows in small things: washers matched to specific torque values, hot-dip galvanizing measured in microns instead of eyeballed, and a metallurgy lab that pulls samples from every coil. Some factories even keep a “failure wall” where bent purlins and cracked brackets from destructive tests are displayed, so new engineers learn what actually breaks. This quiet obsession with reliability is why certain Chinese manufacturers have become default choices for developers in Australia, Chile, and the Middle East, places where a mounting failure is not a warranty headache but a safety event.
Export-ready factories earn that label through more than a UL or CE stamp. They’re the ones whose packing lists match what arrives in Hamburg or Houston, whose pre-assembly guides assume a non-Chinese crew with limited tools, and whose project managers respond to a foundation tolerance question within a day, not a week. Their supply chain advantage is boring but real: in-house roll-forming means a design tweak from 2.0 mm to 2.3 mm doesn’t trigger a three-week requote; direct relationships with local fastener and bearing suppliers keep torque consistency high; and a stockpile of common post sizes lets them ship a pilot order while your full container is still in production. Perhaps most important is scalability. The factory worth a long-term relationship will show you its production schedule without being asked, walk you through how they flex from 20 MW to 200 MW in a quarter, and offer to co-develop a racking variant for your local wind zone rather than forcing a standard SKU. In the end, the best Chinese ground-mount factories aren’t vendors—they’re the quiet engineering partners behind the solar boom.
Contact Us
Contact Person: Nancy
Email: [email protected]
Tel/WhatsApp: +86-13365923720
Website: https://www.topfencesolar.com/