Chocolate Moulding Machine Exporter Guide to Finding a Trusted Supplier
2026-11-16
Choosing a chocolate moulding machine exporter shouldn't feel like gambling your entire production schedule on a handshake. Too many buyers only discover the real supplier after deposits clear—when spare parts vanish, manuals stay untranslated, and '24/7 support' becomes a voicemail in another time zone. Before you sign anything, use this guide to pressure-test every shortlisted exporter. It walks through what actually matters: frame rigidity, PLC stability, demoulding consistency, and the service network behind the brand. If a manufacturer like GUSU can answer the hard questions without dodging, you're already ahead of most buyers looking for a trustworthy partner.
What Exporters Leave Off the Spec Sheet for Chocolate Moulding Lines
Most spec sheets proudly list cavity counts, cycle times, and theoretical output per hour, but they quietly skip the thermal quirks of different mould materials. Polycarbonate, aluminium, and silicone each respond to cooling tunnel temperatures in their own way, and a line tuned for one chocolate formulation can start sticking or ghosting when you switch to a higher cocoa butter content. Exporters rarely mention that the same demoulding air pressure works fine at 22°C but fails miserably at 26°C, leaving you to discover this on your own production floor.
Another convenient omission is the true cost of cleaning and changeover. A spec sheet might say a mould change takes fifteen minutes, but that assumes two technicians, all tools laid out, and no residual chocolate hardened in the corners. In practice, a line with a complex vibrating section or a multi-zone cooling tunnel can eat up two hours per flavour change, and the recommended cleaning agents are often not listed at all. Exporters rarely account for the downtime caused by stubborn cocoa butter residue on conveyor belts or the need to recalibrate sensors after every washdown.
Energy consumption is usually given as a single kilowatt rating for the main drive, which hides the fact that the compressed air system, water chiller, and dehumidifier often draw more power than the moulding line itself. If your factory sits in a humid coastal area, the spec sheet will not tell you that the demoulding efficiency drops sharply above 60% relative humidity, or that you need an extra air dryer sized for peak summer conditions. These operational realities are left for the buyer to stumble into after installation, when the exporter is already on to the next contract.
The Factory Floor Questions That Reveal a Supplier’s Real Capacity
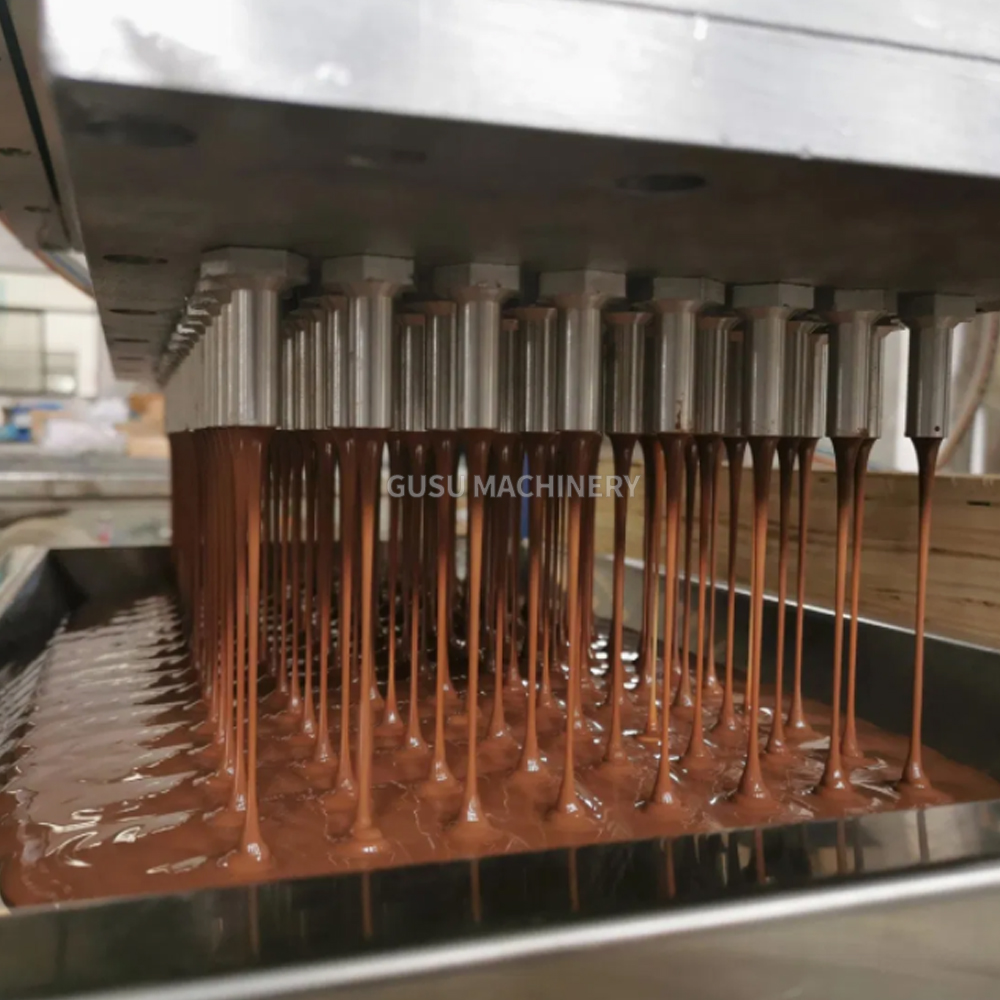
A supplier can recite capacity numbers from a spreadsheet all day, but the assembly line tells a different story. Ask the shift supervisor which workstation creates the most rework, then watch what happens when you stand there for ten minutes. If the answer is vague or the pace slows the moment you leave, capacity is already being stretched in ways the planning sheet won’t show.
On the floor, a few pointed questions cut through polished capability statements: "What percentage of these machines ran a full shift last week?" and "Where are the bottlenecks when two large orders overlap?" The useful answers rarely come from managers alone—ask a line operator how often they wait for materials, or how they handle rush jobs without disrupting standard runs. Real capacity shows up in those pauses, shortcuts, and workarounds, not in theoretical output per hour.
Finally, compare what you hear with what you see. Count the finished goods staged for shipment against the promised weekly volume, and look for obsolete stock tucked in corners—that inventory often hides previous overcommitments. If the floor layout has no room to add a third shift or temporary line, the supplier’s growth claims are probably optimistic. These observations tell you whether the factory can truly absorb your order or just shuffle it around until something else slips.
CE Marks, ISO Claims, and Other Paperwork Worth Verifying
Many buyers assume a CE mark or an ISO certificate is enough. It isn't. Counterfeit paperwork is common, and a glossy PDF proves nothing. Ask for the certificate number, the issuing body, and the specific standard or directive it covers. Then check those details against official databases or the notified body's registry.
An ISO 9001 certificate for a sales office doesn't tell you anything about the factory that actually makes your product. Always match the name and address on the certificate to the entity shipping the goods. Any mismatch—even a missing comma or a different legal suffix—is a red flag, not a trivial typo.
Other documents deserve the same scrutiny: declarations of conformity, test reports, material safety data sheets, and even the packing list. Look for inconsistencies in dates, signatures, and product descriptions. When a supplier pushes back on verification, treat that resistance as information. Legitimate manufacturers rarely hesitate to provide traceable references.
How to Spot a Rebadged Machine Before It Reaches Your Floor
Spotting a rebadged machine often starts with the serial plate. Genuine equipment carries a manufacturer's own badge, stamped or etched with consistent typography and a traceable production code. Rebadgers typically replace this with a generic sticker or a poorly aligned metal tag, sometimes leaving faint outline marks from the original plate underneath. If the brand name looks like it was applied after painting—check for uneven spacing, mismatched screws, or a slightly different shade of paint around the badge area—it's a strong signal the machine didn't leave the factory under that label.
Wiring and internal components tell an even clearer story. Open the electrical cabinet and look for harnesses with zip ties that don't match the machine's age, or connectors that have been cut and spliced with different colored wires. Original builders use consistent looms and label every terminal. A rebadged unit often has multiple generations of wire, generic relays mixed with name-brand PLCs, and software parameters that reference another company's default settings. Check the controller's boot screen or error logs for an unfamiliar OEM name—those hints rarely get wiped completely.
Documentation is the quiet killer. Ask for the original purchase order, maintenance logs, or even the shipping manifest from the first owner. Rebadgers rarely reproduce a full service history, and the manual they hand over may be a photocopy with the original manufacturer's name whited out. Compare the machine's actual component serial numbers—pumps, motors, drives—against the paperwork. If they belong to a different brand or have been ground off and restamped, walk away. A legitimate rebuild will proudly show its lineage, not hide it.
Negotiating After-Sales Support That Survives the First Breakdown
The real test of any after-sales agreement isn't the polished demo or the enthusiastic handshake—it's what happens when the machine halts at 3 a.m. on a Tuesday. Too many contracts read like wishful thinking, promising response windows that dissolve under the pressure of a single critical failure. To negotiate support that actually holds, start by mapping failure scenarios before signing anything. Ask the vendor to walk through a simulated breakdown: who answers the call, what parts are stocked locally, and how quickly can a technician be on-site when the line is down? If they can't articulate that path in concrete terms, the support is theoretical.
One often-overlooked lever is the definition of "critical" itself. Vendors love to attach premium pricing to every possible fault, but a well-negotiated agreement tiers incidents based on operational impact. A sensor glitch that slows output is not the same as a seized spindle that stops production entirely. Insist on precise language for each severity level, and tie financial penalties directly to missed thresholds—not as a punishment, but as a forcing function for the vendor to prioritize your downtime. This shift turns vague promises into measurable obligations.
Finally, build in a review clause that triggers after the first major incident. The first breakdown is rarely a single event; it's a sequence of miscommunications and delayed parts. Negotiate a mandatory post-incident audit where both parties revisit response times, root causes, and spare part availability. This isn't about blame—it's about recalibrating the agreement while the pain is still fresh. If the vendor resists such a clause, that's a warning sign stronger than any line item in the warranty.
Red Flags in Payment Terms That Signal a Vanishing Supplier
Suppliers that demand full payment upfront while refusing to provide verifiable trade references or a physical business address often vanish once funds clear. Legitimate vendors typically accept staged payments tied to milestones or offer escrow options for first-time transactions. When a supplier insists on wire transfers to personal accounts or overseas shell companies without a paper trail, treat it as a loud warning. Genuine businesses want repeat orders, so they avoid terms that destroy trust before delivery.
Another pattern worth watching is a sudden shift from standard net-30 or net-60 terms to cash-on-delivery or 50% deposit requests, especially after months of normal trading. Fraudulent operators use this to extract maximum cash before disappearing. Also note when the payment beneficiary name changes without explanation, or when invoices arrive from a different entity than the one you contracted with. These inconsistencies often indicate a supplier planning an exit.
Finally, be wary of discounts that expire within hours and pressure to pay outside the invoice system. Scammers create artificial urgency to bypass your accounting controls. Before sending money, confirm the bank account details through a separate channel, such as a phone call to a known number. A supplier that avoids video calls, refuses to share utility bills, or cannot name local clients likely has no intention of fulfilling the order.
FAQ
Skip the glossy brochures and ask what type of chocolate they actually have experience with. A supplier who mainly builds moulding lines for solid bars may struggle with one-shot deposited filled chocolates or high-viscosity gianduja. Request at least three running installations in your product category, and ask for the production manager's contact details rather than just the sales reference.
Insist on a live video walkthrough of the exact machine you plan to buy, with the serial number shown on camera. Have the engineer run a mould change and demonstrate the temperature curve from the depositor head to the cooling tunnel outlet. If they hesitate to show a thermal imaging check or refuse to let you speak to the operator, walk away. Third-party inspection through SGS or Bureau Veritas is also worth the cost for a first order.
CE marking and ISO 9001 are the basic entry ticket for most markets, but they do not prove food safety. Check that all product-contact parts are made of food-grade stainless steel or approved plastics, and ask for FDA or EU food contact compliance documents for gaskets and mould materials. If you run organic or allergen-free lines, request documentation that the frame design prevents cross-contamination around drive chains and bearings.
A vague quotation that lists only total price and delivery time is a big warning sign. Reliable exporters break down the scope into machine, moulds, conveyor, cooling tunnel, electrical panel, and spare parts. Also be careful if they demand 100% upfront payment, refuse to share a recommended spare parts list for the first two years, or answer every technical question with 'no problem' but never provide a drawing or data sheet.
Do not compare only the bottom line. Ask each supplier to quote the same specifications: hourly capacity at a specific mould size, type of heating system for the depositor, number of cooling zones, and energy consumption in kW per ton of finished chocolate. Then ask them to list what is excluded, such as moulds, electrical cabling from the main panel to the machine, or commissioning travel costs. A slightly higher price often includes a second set of moulds and a local training visit.
At minimum, you need 24-hour remote diagnosis via video call and a clear commitment on spare part dispatch. Ask how many heating elements, pneumatic cylinders, and PLC modules they keep in stock for your model, and whether they can ship within 48 hours by air if your line stops. Also check if they provide a step-by-step troubleshooting manual in English, not just an installation guide, and whether they can connect you with a technician who speaks your language.
Direct manufacturers usually respond faster to design changes and give you clearer technical answers, but some trading companies are excellent at bundling a moulding line with wrapping machines and cooling tunnels from different factories. If you choose a trading company, ask them to reveal the actual manufacturer's name and factory address before signing. A trustworthy trader will agree to a three-party contract where the manufacturer remains responsible for the core warranty.
Confirm the incoterm carefully. DAP or CIF might look easy, but you need to know if the price includes fumigated wooden crates, moisture-proof wrapping, and lifting point markings. Before shipment, request a foundation drawing and a leveling procedure. For installation, many exporters offer remote guidance, but a two or three-day on-site commissioning visit is worth negotiating because small misalignments in the chain or mould guide rails can cause weeks of headaches later.
Conclusion
When sourcing chocolate moulding lines, the glossy brochure never tells the whole story. Many exporters quietly omit details that matter on your production floor—things like actual cycle time at full mould depth, changeover tolerances for different chocolate viscosities, or whether the quoted throughput assumes a perfectly tempered supply. Ask for a live demonstration with your own chocolate, not just a video of pralines gliding along. On the factory floor, probe beyond the polished showroom: how many identical lines have they shipped in the last twelve months? Can they give you contact details for two buyers running the same configuration? That conversation often reveals more than any datasheet. Then, before you trust the CE mark or the ISO certificate on the wall, verify the paperwork. Request the technical file, the declaration of conformity number, and cross-check it with the notified body. A surprising number of certificates are expired, borrowed, or belong to a different machine category. If the supplier hesitates to share those documents, treat that pause as a warning.
Rebadged machines are more common than many buyers realise. The giveaway is usually in the control cabinet: mismatched PLC brands, handwritten wire labels, or a frame serial number that doesn't match the manual. Ask which components are actually produced in-house versus sourced, and have them point to the casting marks on the main frame—if the paint looks factory-fresh but the bolts show wear, you're likely looking at a refurbished unit passed off as new. After-sales support is where the real relationship gets tested. Don't settle for a promise of "24/7 support"; ask for a named engineer, a guaranteed response window, and a written escalation path that survives the first breakdown. Many exporters go silent after the second email. Finally, watch the payment terms. A supplier demanding 70% upfront with the balance against a bill of lading you cannot verify, or asking for payment to an offshore account that doesn't match the company name, is signalling trouble. Use an escrow or letter of credit tied to a third-party inspection at the port of loading. If they refuse, walk away.
Contact Us
Contact Person: Zhang Wei
Email: [email protected]
Tel/WhatsApp: 8618662577837
Website: https://www.chocomachinery.com