Best Plastic Shredder for Efficient Plastic Recycling at Any Scale
2026-09-25
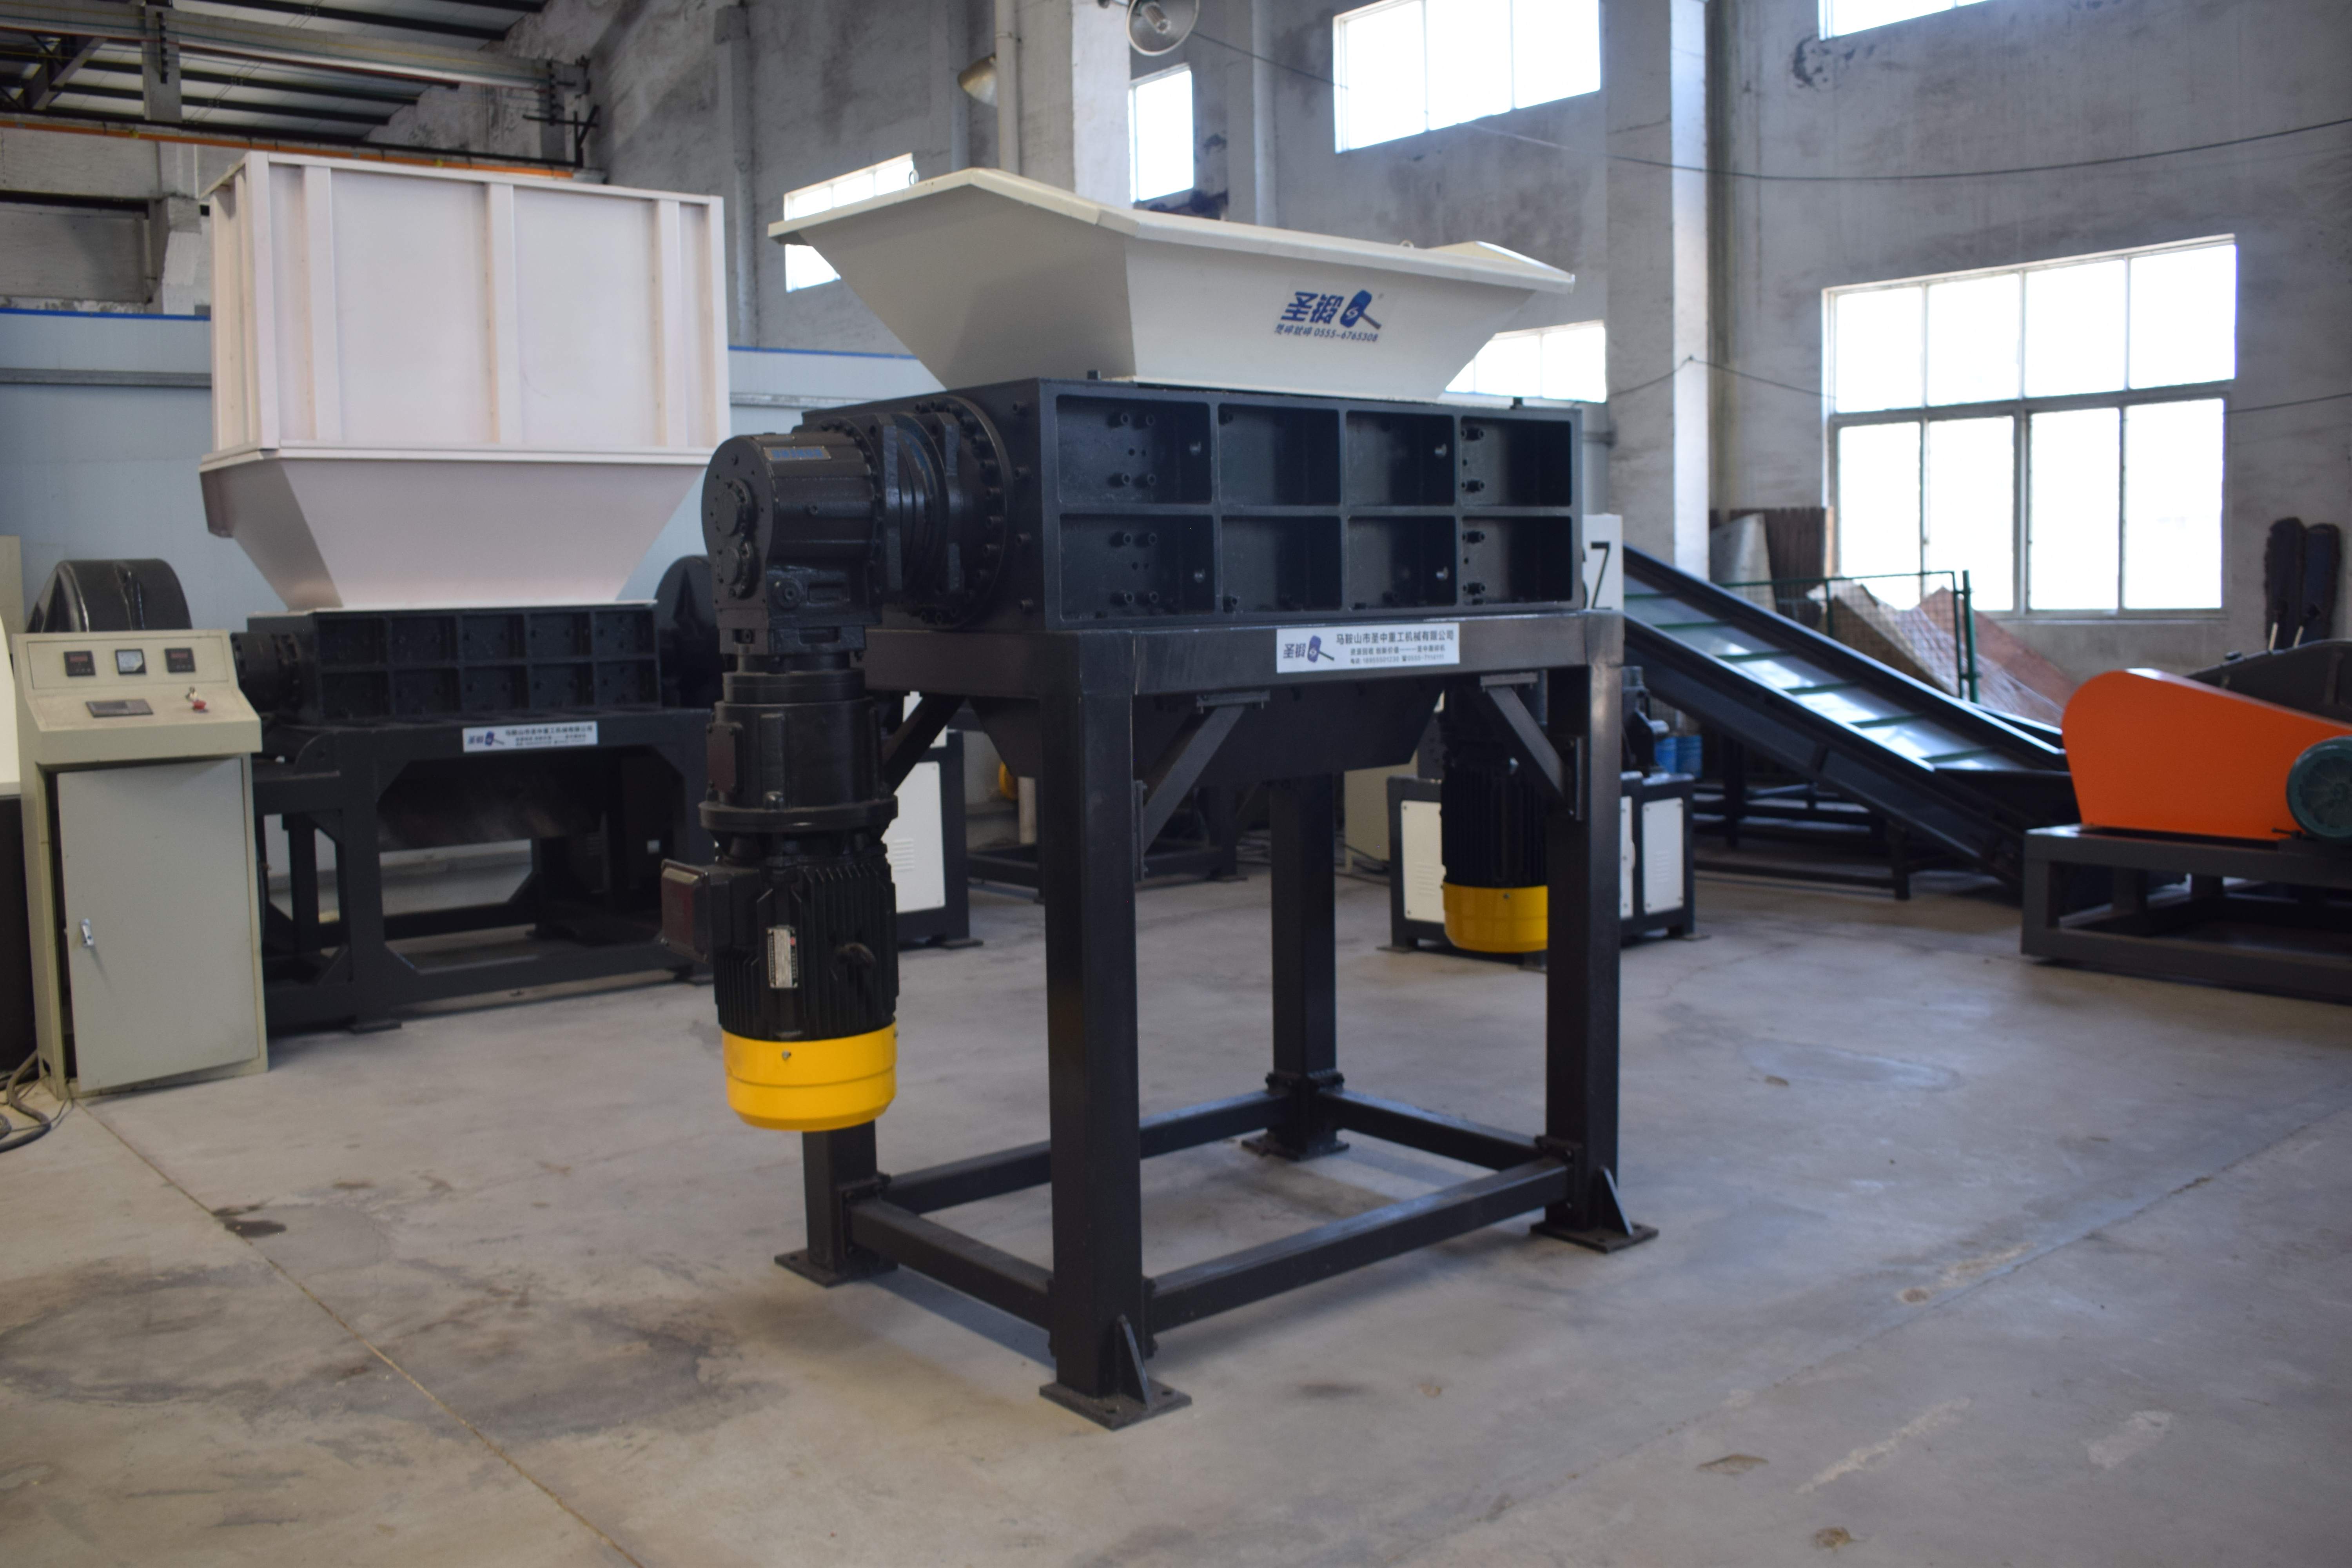
From small workshops to high-volume recycling plants, the right plastic shredder can make or break your operation. Most machines either choke on thick scrap or waste energy on light film—but what if one shredder could handle both without slowing down? In this guide, we break down what to look for at every scale and why Shengzhong Shredder keeps showing up as the practical choice for recyclers who need consistent output. Whether you are processing post-industrial purges, bottles, or bulky lumps, the next few sections will help you match the machine to the job before you invest.
What Actually Happens When Plastic Hits the Blades?
The first contact is rarely a clean slice. A rotating blade catches an edge or a thin wall, flares it, and then tears through. Because most plastics are viscoelastic, they stretch slightly before they fracture, especially in warmer operating conditions. That produces heat at the cutting edge. Enough repeated impacts can soften the material just ahead of the blade, leading to smearing or melting instead of a crisp cut.
If the plastic is rigid, like a chunk of ABS or a thick HDPE puck, the blade may chip a small fragment loose before the main crack propagates. These micro-cracks radiate outward, and depending on blade speed and tip sharpness, the part can shatter into angular flakes or peel away in long spirals. A dull blade changes the outcome entirely: instead of cutting, it compresses the plastic, builds friction, and can weld a thin film onto the blade face. That film reduces clearance and makes each subsequent impact hotter and less effective.
Matching Shredder Size to Your Real Volume Without Overspending
Most offices overestimate how much paper actually hits the bin in a day. A shredder rated for 20 sheets per pass sounds impressive until you realize you rarely feed more than five at once, and the motor spends most of its time idling. Start by tracking what you shred over a normal week—junk mail, drafts, a few client files—not the worst-case backlog you clean out twice a year.
Sheet capacity is only half the story. A machine with a 10-sheet rating but a 30-minute continuous run time will handle a daily stack far better than a 20-sheet model that needs to cool down after six minutes. Match the duty cycle and bin size to your rhythm: if shredding happens in short bursts between calls, a smaller, quieter unit does the job without dominating the desk or the budget.
Spending more for a bigger throat or cross-cut particles you don't need rarely pays off. Unless you're destroying sensitive HR or legal documents, strip-cut or micro-cut may be overkill. Buy for the volume you actually push through in a typical session, not the capacity printed on the box, and you'll get years of reliable use without paying for idle horsepower.
The Hidden Costs of Cheap Plastic Shredders No One Mentions
Most buyers fixate on the sticker price of a budget plastic shredder, but the real expense creeps in through premature blade wear. Cheap units often use low-grade steel that dulls after a few hundred pounds of material, forcing replacements that cost nearly as much as the machine itself. Unlike industrial models with hardened, replaceable cutters, these entry-level shredders treat blades as disposable—yet rarely advertise that fact.
Then there's the overlooked energy drain. A poorly engineered motor draws more current under load, spiking your electricity bill with every batch of hard plastics like HDPE or ABS. Over a year of regular use, that inefficiency can add up to the price difference between a cheap shredder and a mid-range one—quietly erasing any initial savings.
Maintenance downtime is the third hidden cost no spec sheet mentions. Jams from weak gearboxes, overheating after twenty minutes of continuous feed, and clogged screens that require full disassembly all eat into your productive hours. For a small recycling workshop, that lost time translates directly into missed orders or delayed projects—an expense that never appears on the invoice but hits the bottom line harder than the purchase price ever did.
How to Keep a Plastic Shredder Running Without Constant Jams
Most jams in a plastic shredder trace back to how material enters the cutting chamber. Instead of dumping a full bin at once, feed pieces steadily and use a pusher to keep light items in contact with the rotor. If you're handling large containers or purgings, pre-cut them into slabs no wider than the rotor opening. A simple trick is to layer soft films between harder chunks so the rotor doesn't grab a thick rigid piece and stall.
Blade condition matters more than people expect. Dull knives force the motor to work harder and often regrind the same material until it heats up and clogs the screen. Check rotor and bed knife clearance every few weeks, and touch up edges before they become rounded. A clean screen is just as important; wipe it down or brush out the holes after each shift, especially if you shred sticky plastics like HDPE or PET bottles.
Sorting before shredding prevents many mid-run stops. Remove metal bands, nails, or even dirt-caked labels that can wedge between the rotor and housing. For wet or washed plastics, let them drain completely, as moisture makes film cling and reduces throughput. Finally, match the shredder to your material mix: a low-speed, high-torque machine handles thick purgings better, while a high-speed granulator needs smaller, more uniform feed to avoid jamming.
Which Plastics Are Worth Shredding (and Which Just Waste Energy)
Not every plastic deserves a turn in the shredder. Rigid, high-value thermoplastics like HDPE, PP, and ABS break down into clean, reusable flakes with minimal energy input. These materials hold their mechanical properties through multiple grinding cycles, making them ideal candidates for closed-loop recycling. On the other hand, thin films, foam, and heavily contaminated packaging often create more problems than they solve. They wrap around rotors, generate excessive fines, and demand extra washing and drying that consumes more power than the recovered material is worth. A quick pinch test usually tells the story: if the plastic springs back or tears like a grocery bag, it's better off in a densifier or waste-to-energy stream than in your granulator.
Mixed plastic waste with unknown additives presents another hidden cost. PVC, for example, can release corrosive chlorine compounds when heated during high-speed shredding, damaging blades and contaminating the entire batch. Similarly, plastics loaded with glass fiber or mineral fillers will dull knives rapidly, turning a cheap processing step into a constant maintenance headache. Smart operators sort by resin type and contamination level before shredding, focusing only on clean, thick-walled items that provide a positive return on energy. Everything else just burns electricity and wears down equipment.
The real art lies in recognizing when shredding adds value versus when it is simply an expensive form of procrastination. A bulky ABS computer housing or a stack of PP buckets? Shred without hesitation—the output sells. But a tangled mess of LDPE stretch wrap or a bin of greasy takeout containers? You are not recycling; you are just making smaller garbage. The energy math rarely lies: if the shredded flake cannot find a buyer at a price above your operating cost, the machine is not doing you any favors.
From Shredded Flakes to Usable Feedstock Without the Usual Bottleneck
The real problem rarely starts at the extruder. It starts in the transition from a bale of washed, shredded flakes to a steady, homogeneous melt stream. Flakes vary in thickness, residual label adhesive, and trapped moisture; if those aren't dealt with before the feed throat, you end up fighting surging, black specks, and pressure swings all shift.
One overlooked fix is to redesign the handling path rather than add more heat. A compact cyclone plus a low-speed agitator can strip out fines and even out bulk density before the material reaches the hopper. Adding a vented pre-dryer that holds flakes at just under their softening point removes trapped water without melting the edges of the flakes together—this alone eliminates most hydrolytic degradation in PET and PA.
Once the fines are gone and moisture is stable, a short, water-cooled crammer feeder can push even mixed flakes into the screw without bridging. Melt filtration then becomes predictable: fewer gels, fewer pressure drops, and screen changes measured in days instead of hours. That is the whole point—not faster extrusion, but fewer interruptions.
FAQ
Focus on a modular design with accessible screens and adjustable rotor speed. If you sometimes process thin film and later move to thick purgings, a variable speed drive lets you dial back torque for noise-sensitive batches. Also check whether the cutting chamber opens without tools; that makes swapping screen sizes for different output fractions a ten-minute job instead of half a day. Machines with bolted-on hoppers tend to be easier to adapt than welded frame units.
Single-shaft models usually give you a more uniform chip size, which helps if the material goes straight into extrusion. Dual-shaft machines tolerate metal contamination and oversized chunks better, but they often produce a coarser, less consistent cut. If your incoming stream has things like pipe fittings or small metal inserts, start with a dual-shaft as a primary shredder and run the output through a granulator later. For clean, sorted plastic, a single-shaft with a well-tuned bed knife does the job with fewer fines.
Keep a log of blade gap checks rather than relying on hours alone. After every 40–60 running hours, measure the clearance between rotor and bed knives; a gap that has drifted by more than 0.1 mm usually means uneven wear or a loosened bolt. Rotate or flip knives before edges look visibly dull, not after. Also clean behind the screen regularly—compacted fines push the screen outward and change the cutting geometry. A quick air blowdown of the motor vents helps too, especially in dusty plants.
Yes, but only if you pre-cut the drums into sections that fit the feed opening without forcing. Many smaller shredders are rated for wall thickness up to 6–8 mm but will stall if a curved drum wall wedges sideways. Feed the pieces flat and use a ram or wooden push block instead of your hands. If the machine has a reverse function, use short reverse pulses the moment the rotor speed drops, rather than waiting for a full stall. Softer HDPE often melts from friction before it cuts cleanly, so a coarse screen and slower feed rate help.
Look for a two-hand start or keyed lockout on the main disconnect, plus an interlock that kills power the moment the hopper lid opens. An emergency stop cable along the frame is more useful than a single button if the machine is longer than a few feet. For any shredder with an open discharge, a magnetic separator or at least a strong plate magnet should be placed downstream to catch stray steel from previous processing. Also insist on a rotor lock pin for blade changes—chocks and wooden blocks are not a substitute.
Blades made from D2 or SKD-11 tool steel hold an edge longer and produce cleaner cuts on rigid plastics, meaning fewer micro-tears that lead to dust and angel hair. For abrasive streams with glass-filled nylon or heavily contaminated material, a harder alloy like DC53 or a coated edge reduces chipping. Softer, lower-cost blades tend to roll the cutting edge after a few weeks, which smears the plastic and creates irregular flakes that bridge in feed throats. Match blade hardness to your dirtiest material, not your cleanest.
If your downstream process is injection molding or profile extrusion, yes. A shredder alone usually gives you chips anywhere from 10 to 40 mm, which can feed a melt extruder but often starve the screw or trap air. A granulator tuned to 6–8 mm gives more consistent bulk density and faster melting. However, the extra stage adds energy, floor space, and another set of knives to maintain. For washing lines or densification, you may skip the granulator and use the shredder output directly.
A 30 kW shredder does not always draw 30 kW. Under a light and steady load, it may run at 40–55% of rated power, so a realistic continuous cost is closer to 12–18 kWh per hour plus peak demand charges. The hidden cost is frequent starts against a full chamber; that can double the amp draw for a few seconds. Use a soft starter or VFD to shave those spikes. Also check your plant's power factor—older motors without correction can add 10–15% to apparent power billing.
Conclusion
A shredder that truly works at any scale has to earn its place by handling the grinder’s reality, not just the spec sheet. When plastic hits the blades, what actually happens is less about horsepower and more about rotor geometry, cutting clearance, and feed control. Cheap units stall or snap because they ignore this, while a well-designed shredder turns mixed rigid plastics, film, and even purgings into consistent flakes without binding. Matching size to real volume means looking at peak surges and material types, not just average throughput, so you avoid overspending on a giant machine that idles most of the shift or underspending on one that chokes every afternoon. Hidden costs of budget shredders show up fast: frequent blade replacements, motor burnouts, and downtime that dwarfs the initial savings. Keeping the machine running without constant jams often comes down to feed rate control, screen selection, and a maintenance rhythm that doesn’t wait for a breakdown.
Deciding which plastics are worth shredding changes the economics entirely. PET, HDPE, PP, and LDPE film generally repay the energy with clean, reusable flake, while heavily contaminated multilayer packaging or brittle thermosets just waste electricity and dull the knives faster. The real bottleneck in many recycling lines isn’t the shredder itself—it’s the step between shredded flakes and usable feedstock. Without proper size reduction, metal separation, and a consistent output size, extruders and wash lines starve or clog. A reliable shredder paired with smart screening and air classification turns that transition into a steady flow, not a firefighting exercise. At any scale, the best choice is one that matches your actual material stream, keeps blade changes quick, and doesn’t demand a dedicated operator just to keep it from seizing. That’s what separates efficient plastic recycling from a noisy, expensive hobby.
Contact Us
Contact Person: Leon
Email: [email protected]
Tel/WhatsApp: 8615385558866
Website: https://www.shred-waste.com